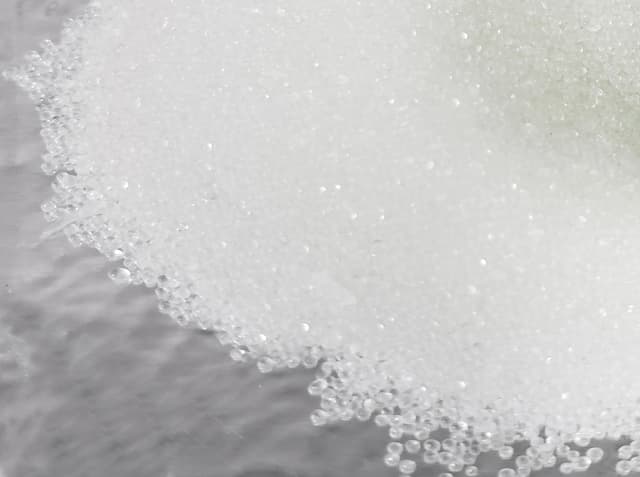
Nucrel 0910 is a copolymer of ethylene and methacrylic acid. The resin is available for use in conventional extrusion and coextrusion equipment.
Extrusion Coating/Lamination
| Extrusion Coating/Lamination | Nominal Values |
|---|---|
| Processing Information | A suggested extruder set temperature profile. |
| Feed Zone | 185°C (365°F) |
| Second Zone | 235°C (455°F) |
| Third Zone | 260°C (500°F) |
| Fourth Zone | 285°C (545°F) |
| Fifth Zone | 285°C (545°F) |
| Adapter Zone | 285°C (545°F) |
| Die Zone | 285°C (545°F) |
General Processing Information
Nucrel 0910 is normally processed at melt temperatures ranging from 260°-305°C (500°-581°F) in flat die equipment. For extrusion coating and laminating, a typical extruder profile is below. Actual processing temperatures will usually be determined by either the specific equipment or substrate or one of the other polymers in a coextrusion. Materials of construction used in the processing of this resin should be corrosion resistant. Stainless steels of the types 316, 15-5PH, and 17-4PH are excellent, as is quality chrome or nickel plating, and in particular duplex chrome plating. Type 410 stainless steel is satisfactory, but needs to be tempered at a minimum temperature of 600°C (1112°F) to avoid hydrogen-assisted stress corrosion cracking. Alloy steels such as 4140 are borderline in performance. Carbon steels are not satisfactory. While stainless steels can provide adequate corrosion protection, in some cases severe purging difficulties have been encountered. Nickel plating has been satisfactory, but experiments have shown that chrome surfaces have the least adhesion to acid based polymers. In recent years, the quality of chrome plating has been deteriorating due to environmental pressures, and the corrosion protection has not always been adequate. Chrome over top of stainless steel seems to provide the best combination for corrosion protection and ease of purging. If surface properties of the extruded resin require modification (such as, lower C.o.F. for packaging machine processing), refer to the CONPOL™ Processing Additive Resins product information guide. After processing NUCREL™, purge the material out using a polyethylene resin, preferably with a lower melt flow rate than the NUCREL™ resin in use. The "Disco Purge Method" is suggested as the preferred purging method, as this method usually results in a more effective purging process. Information on the Disco Purge Method can be obtained from Formula Chemicals. Never shut down the extrusion system with NUCREL™ in the extruder and die. Properly purge out the NUCREL™ with a polyethylene, and shut down the line with polyethylene or polypropylene in the system.
FDA Status Information
Nucrel 0910 complies with Food and Drug Administration Regulation 21 CFR 177.1330(a) - - Ionomeric resins, subject to the limitations and requirements therein. This Regulation describes polymers that may be used in contact with food, subject to the finished food-contact article meeting the extractive limitations under the intended conditions of use, as shown in paragraph (c) of the Regulation.
Regulatory Information
For information on regulatory compliance outside of the U.S.A., consult your Formula Chemicals representative.
Safety & Handling
For information on appropriate Handling & Storage of this polymeric resin, please refer to the material Safety Data Sheet. A Product Safety Bulletin, material Safety Data Sheet, and/or more detailed information on extrusion processing and/or compounding of this polymeric resin for specific applications are available from Formula Chemicals.
Price
Request Quote
Port of Origin: Shanghai
1 Pallet
Compare Products
Physical Data
Density (g/cm³)
0.93
Melting point
100°C (212°F)
Composition
8.7% By Weight Methacrylic Acid comonomer content
Melt Flow Index (190°C/2.16kg)
10.0 g/10 min
Freezing Point (DSC)
82°C (179.6°F)
Vicat Softening Point
81°C (177.8°F)
Maximum Processing Temperature
310°C (590°F)
Applications
Recommended
Limited Suitability
Not Recommended
COATINGS
Automotive Coating
Industrial Coating
Decorative Coating
Coil Coating
Wood Coating
Powder Coating
PLASTICS
PVC
PE/PP/PO
ABS
PS
PA
Rubber
INKS
Offset
Solvent based
Water based
UV / EB
Inkjet
Acrylic
Logistics, shelf life and storage
Port of Origin 1
Shanghai
Shipping Net Kg/Pallet
1000
Pal Length
1.15
Pal Width
1.15
Pal Height
1.15
Lead Time (days)
30
Related Products
Color Index: N/A

Color Index: N/A
